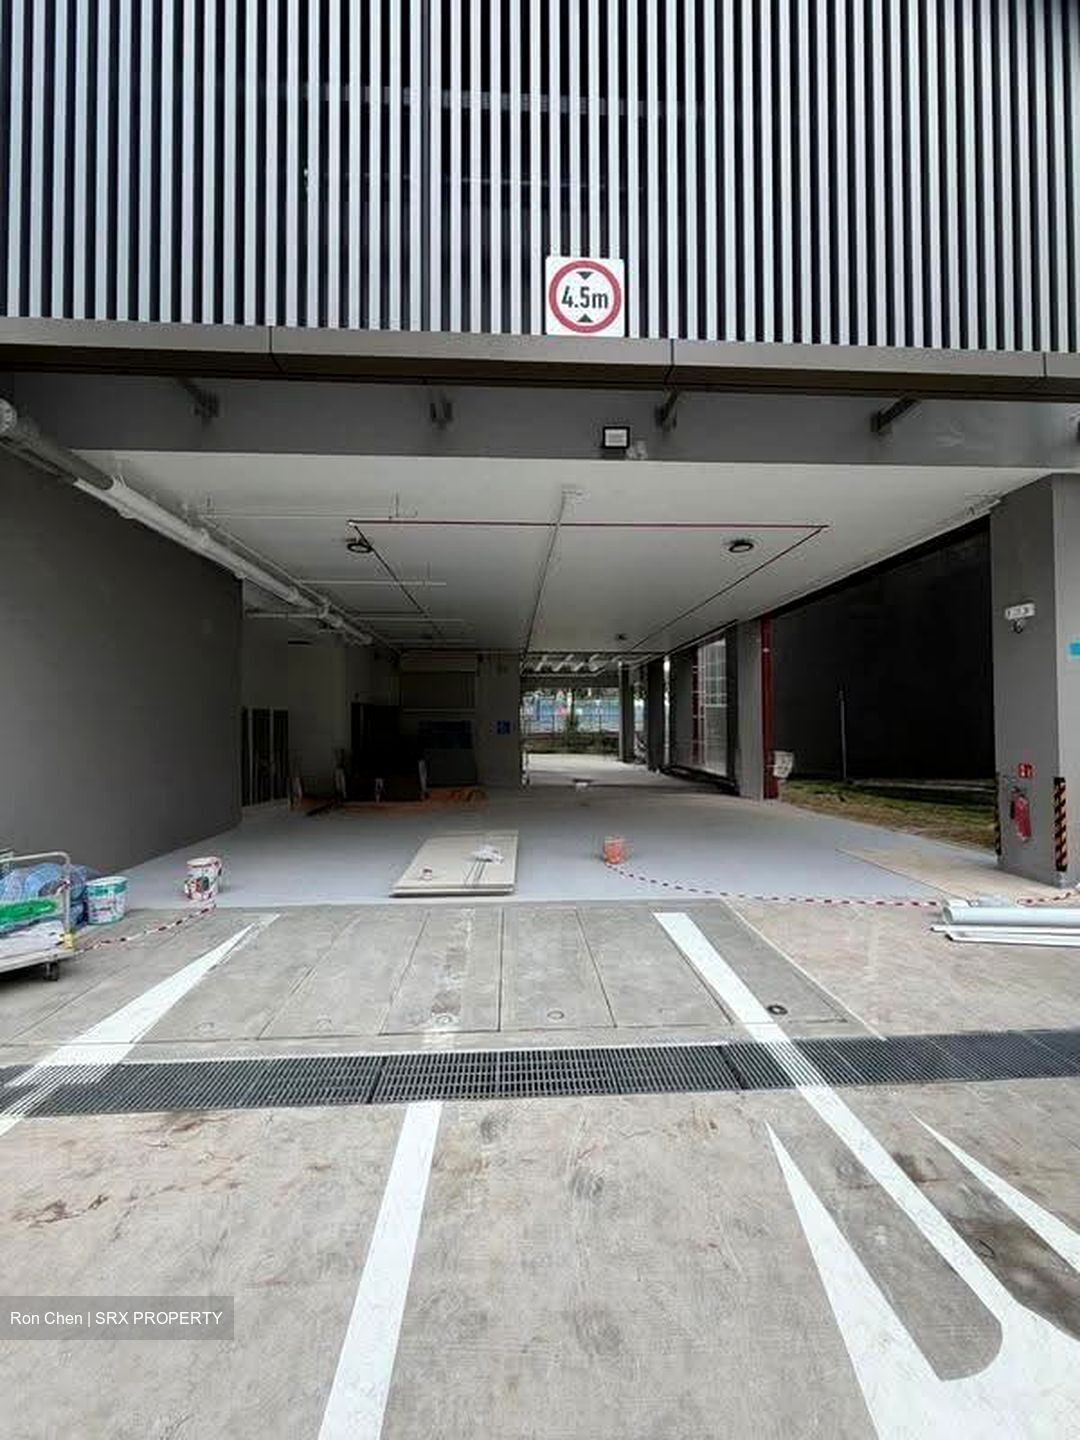
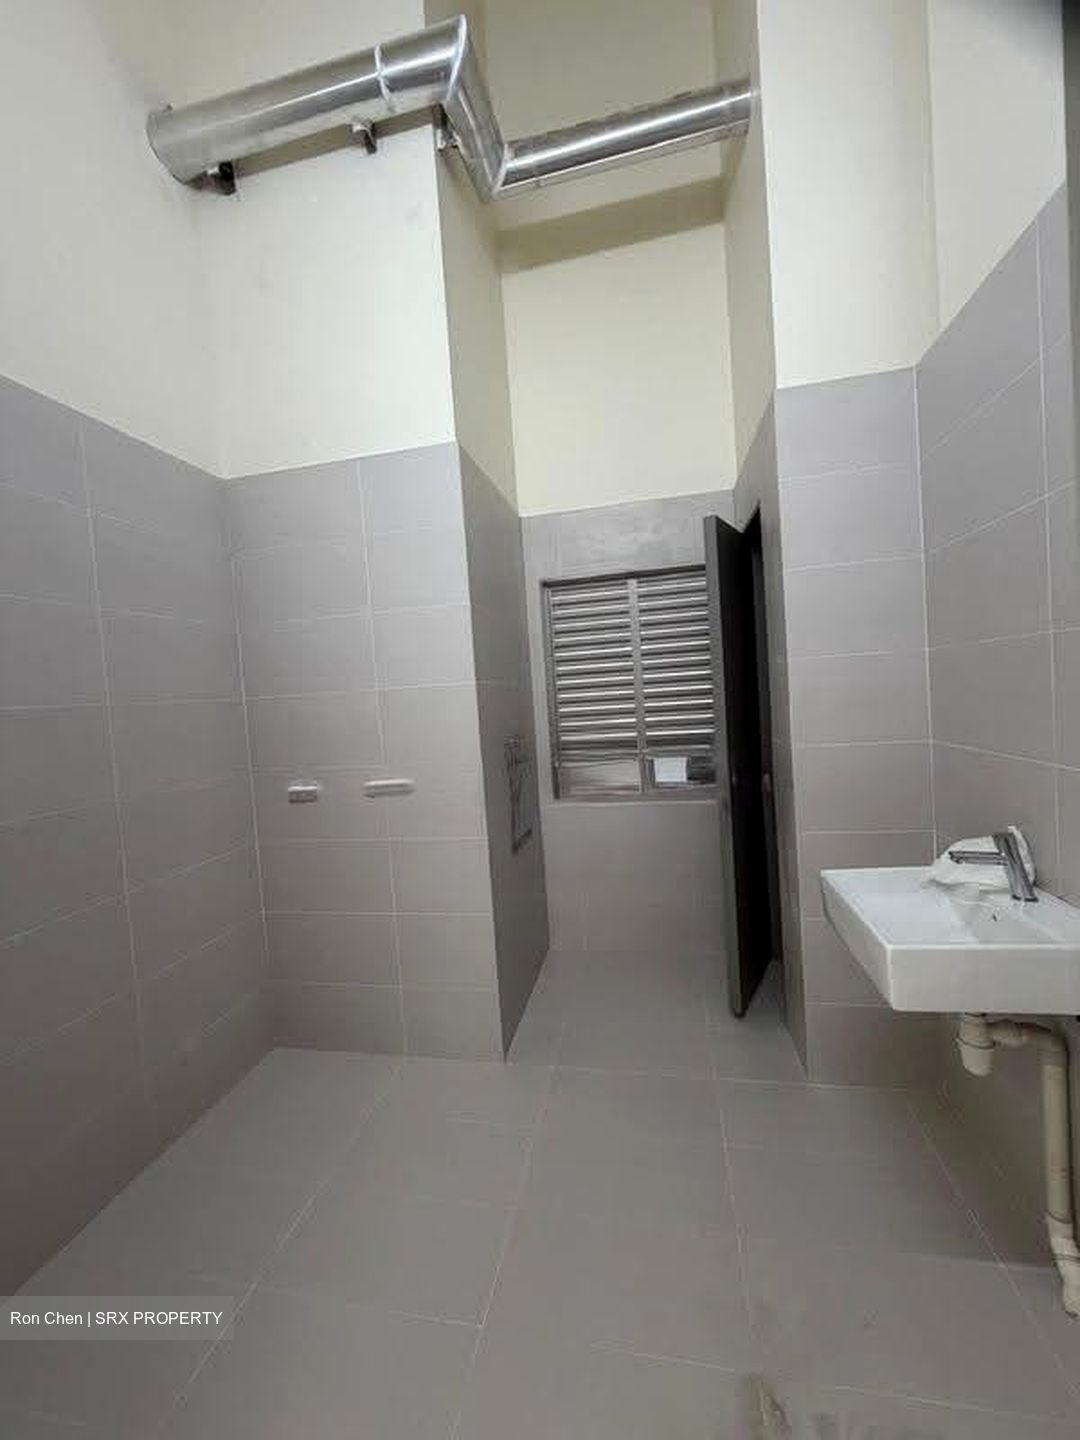
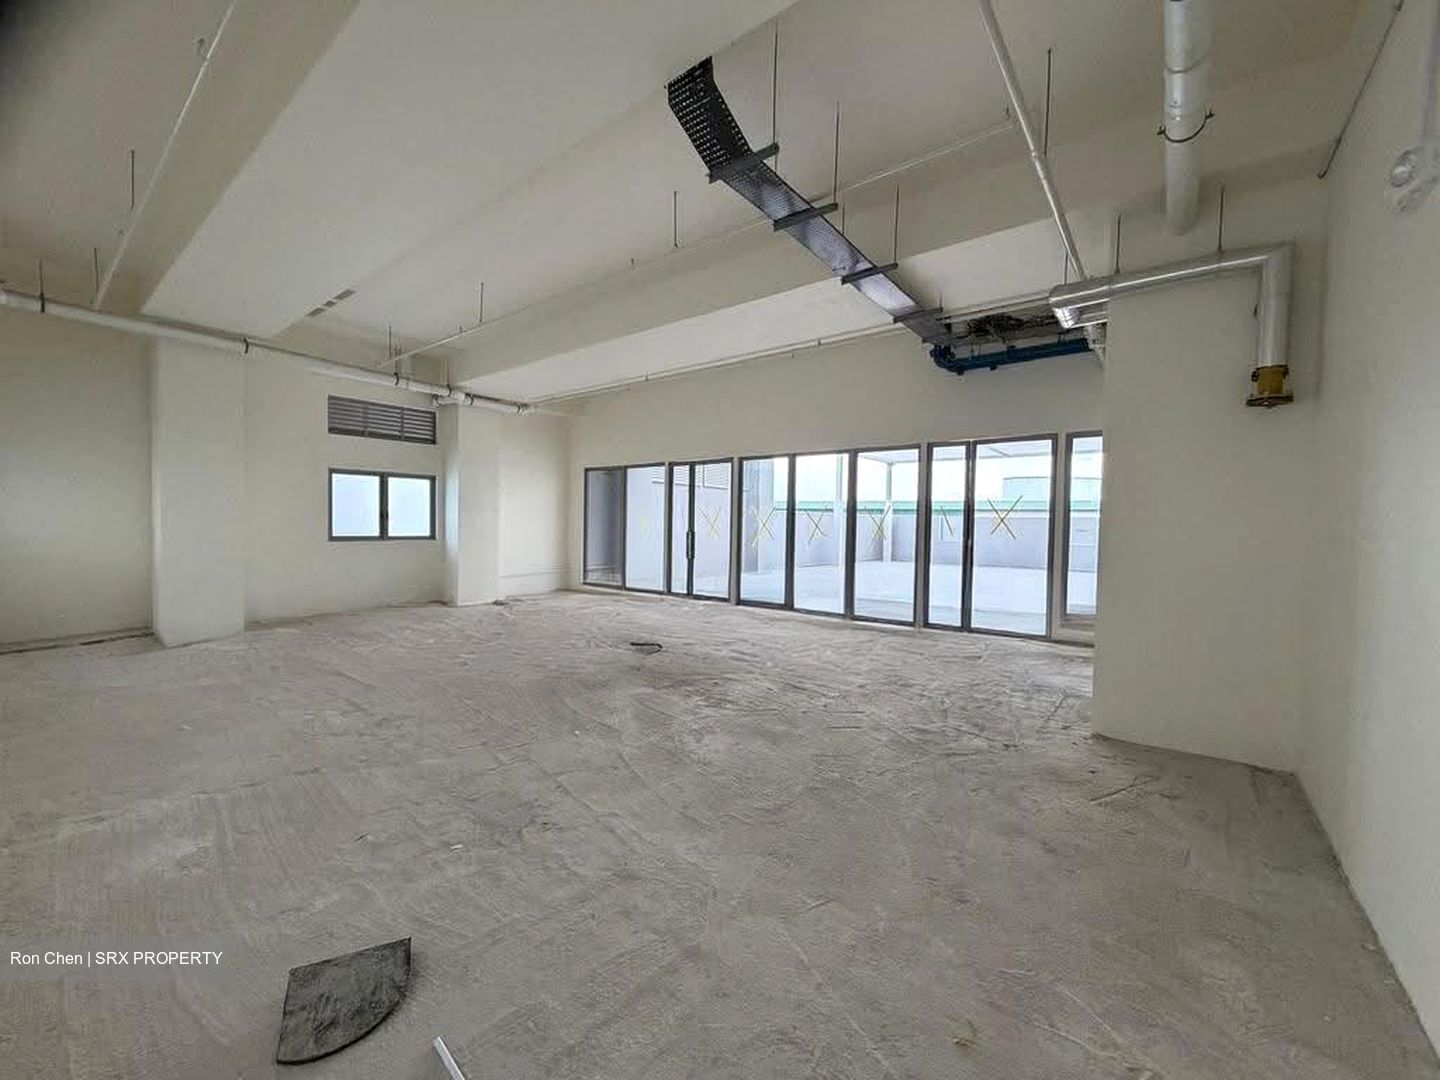
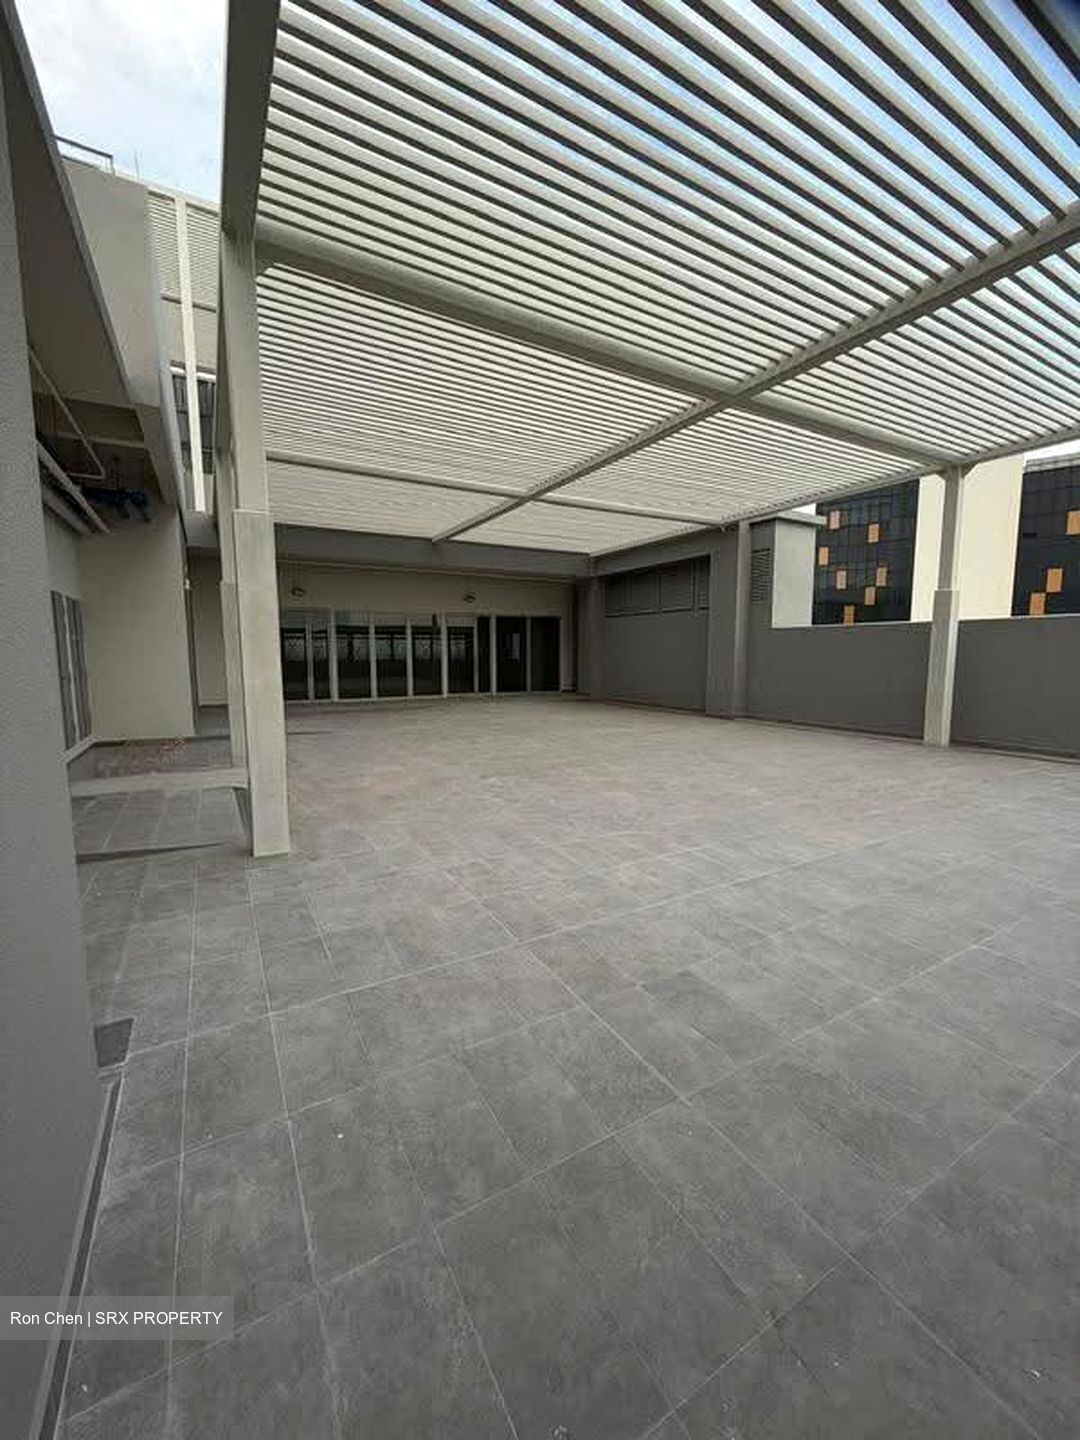
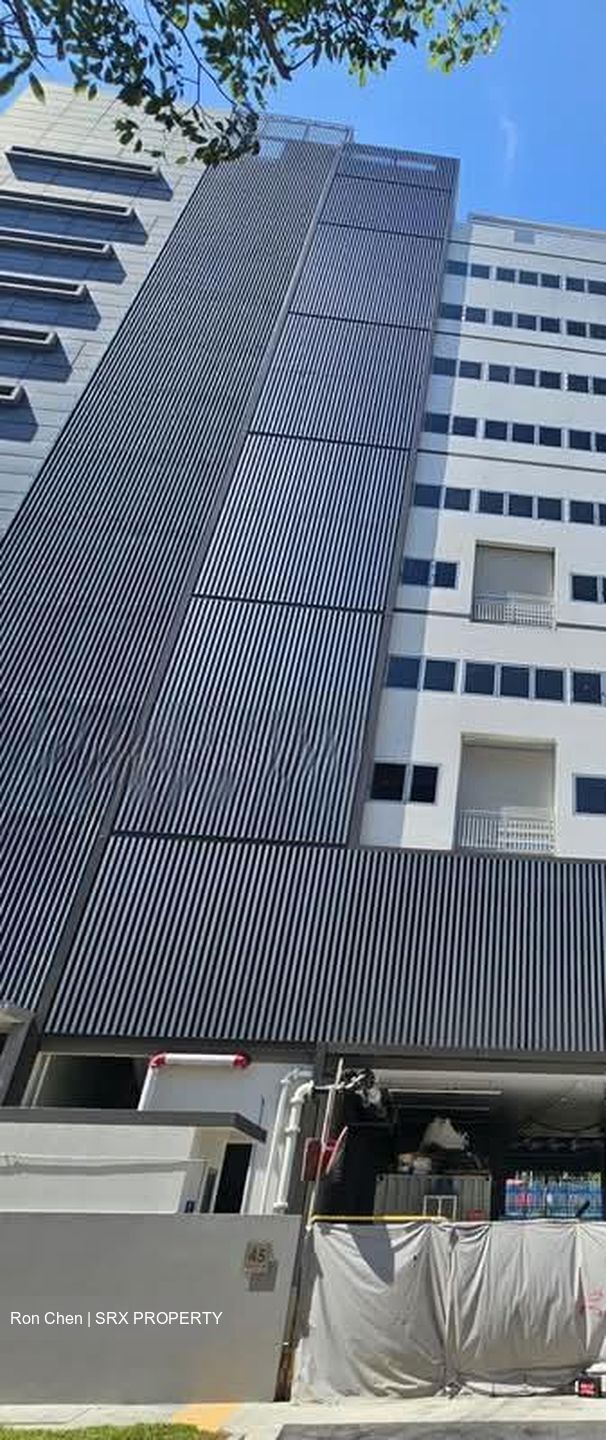
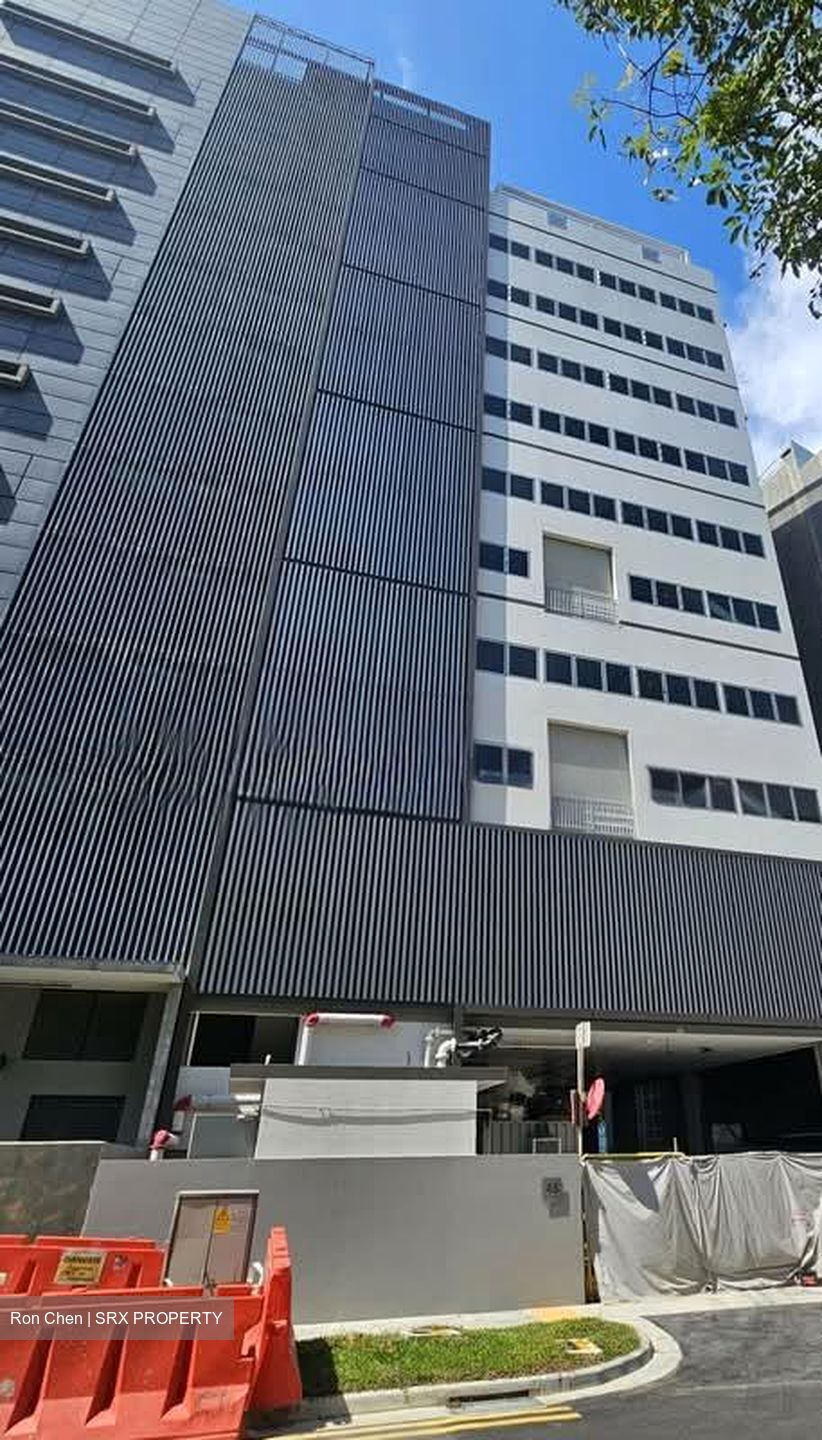
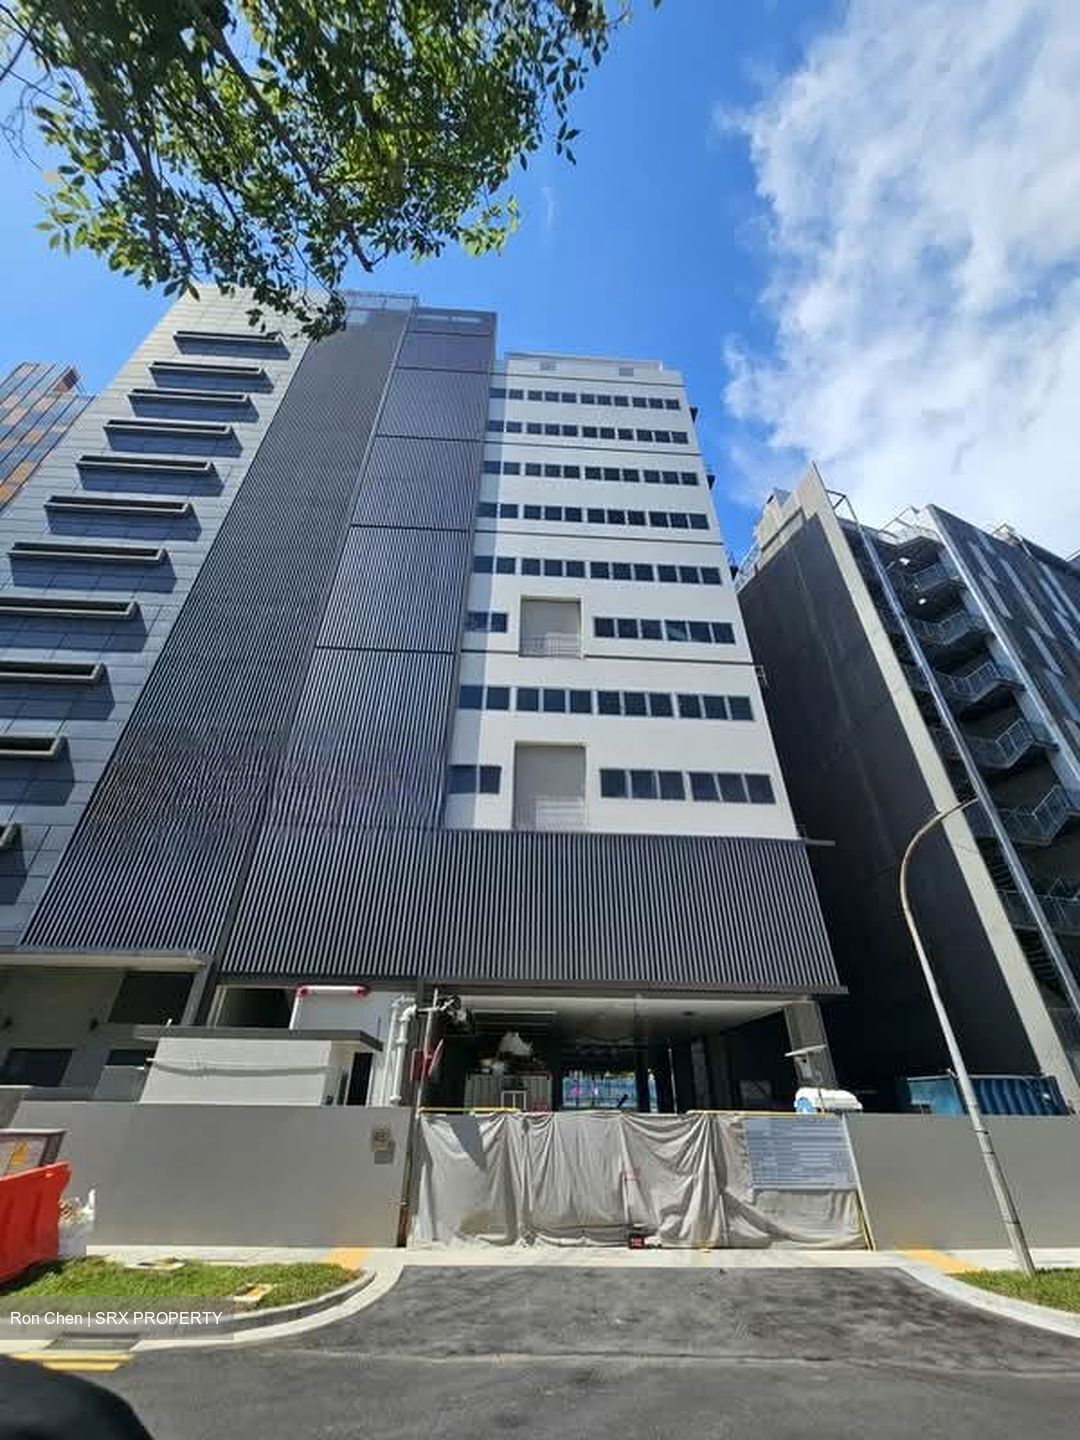
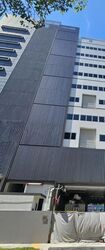
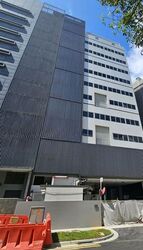
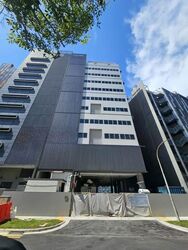
BRAND NEW 6-Storey Purpose-Built Multi-User B2 Food Manufacturing Facility with Ancillary Industrial Canteen
Move In. Fit Out Faster. Produce Sooner.
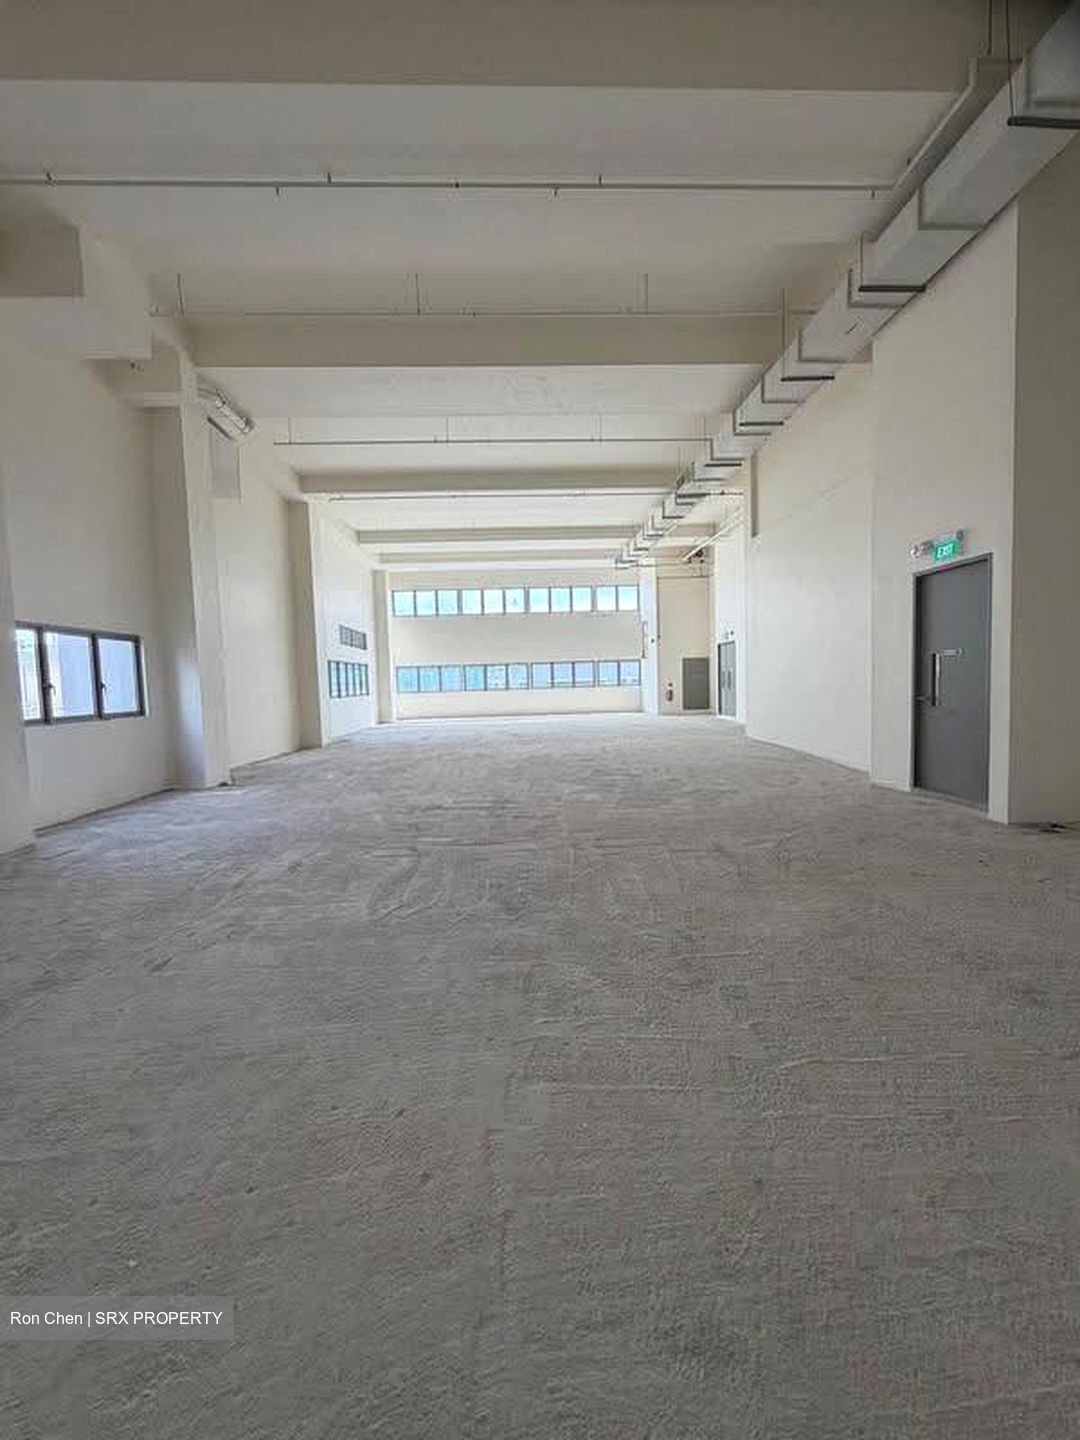
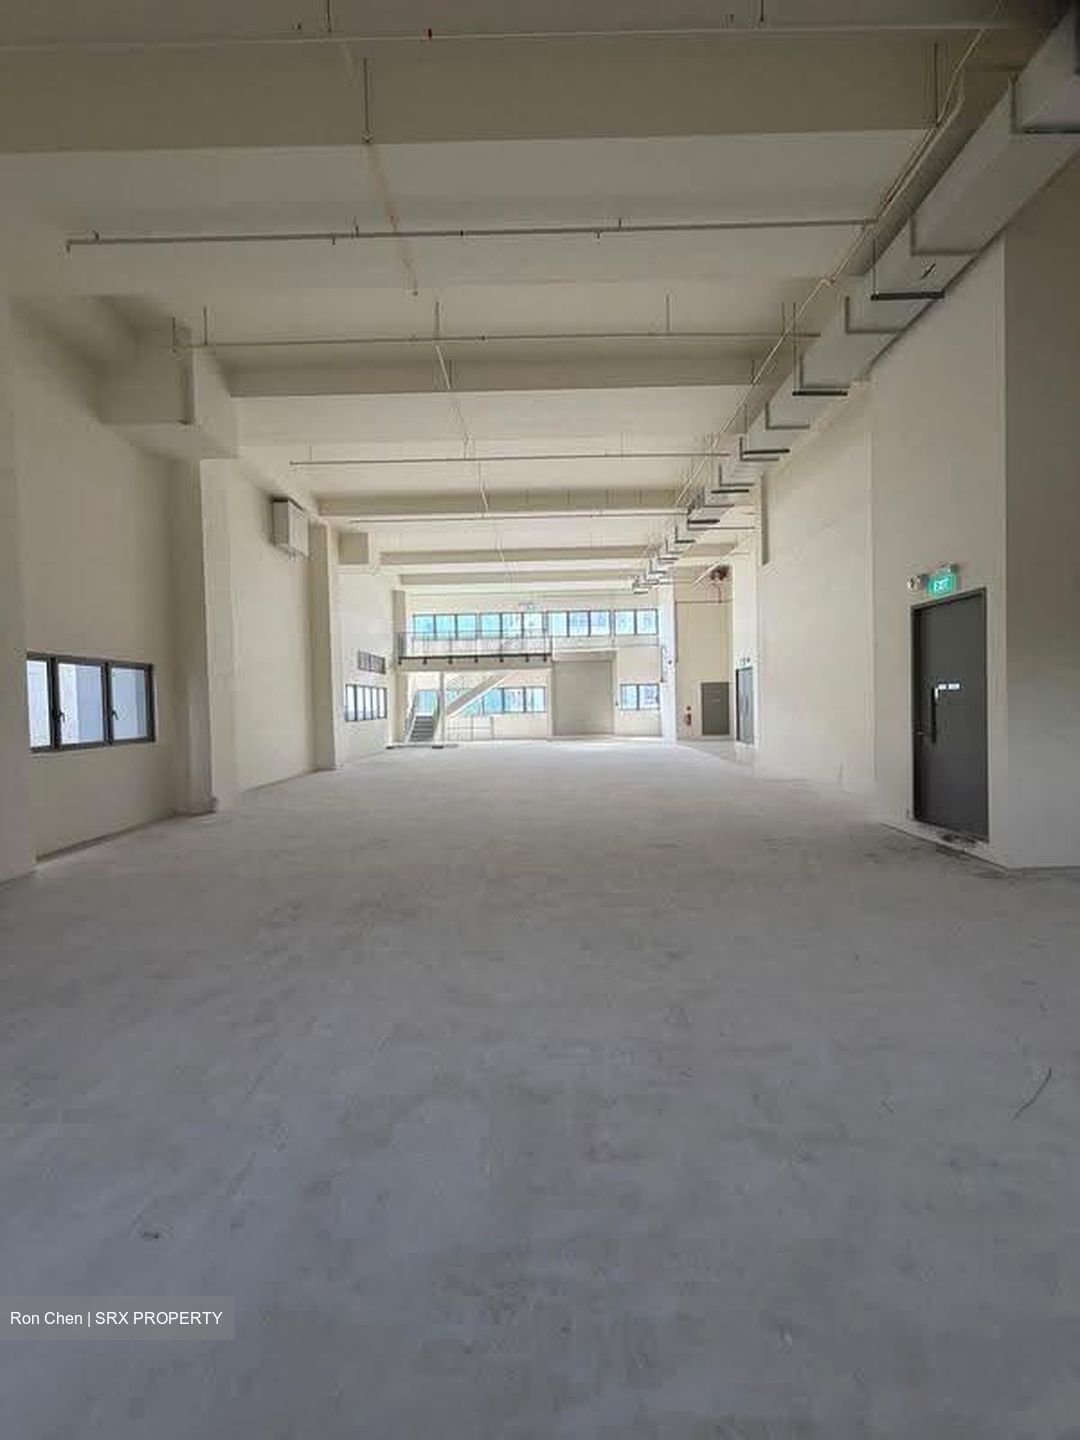
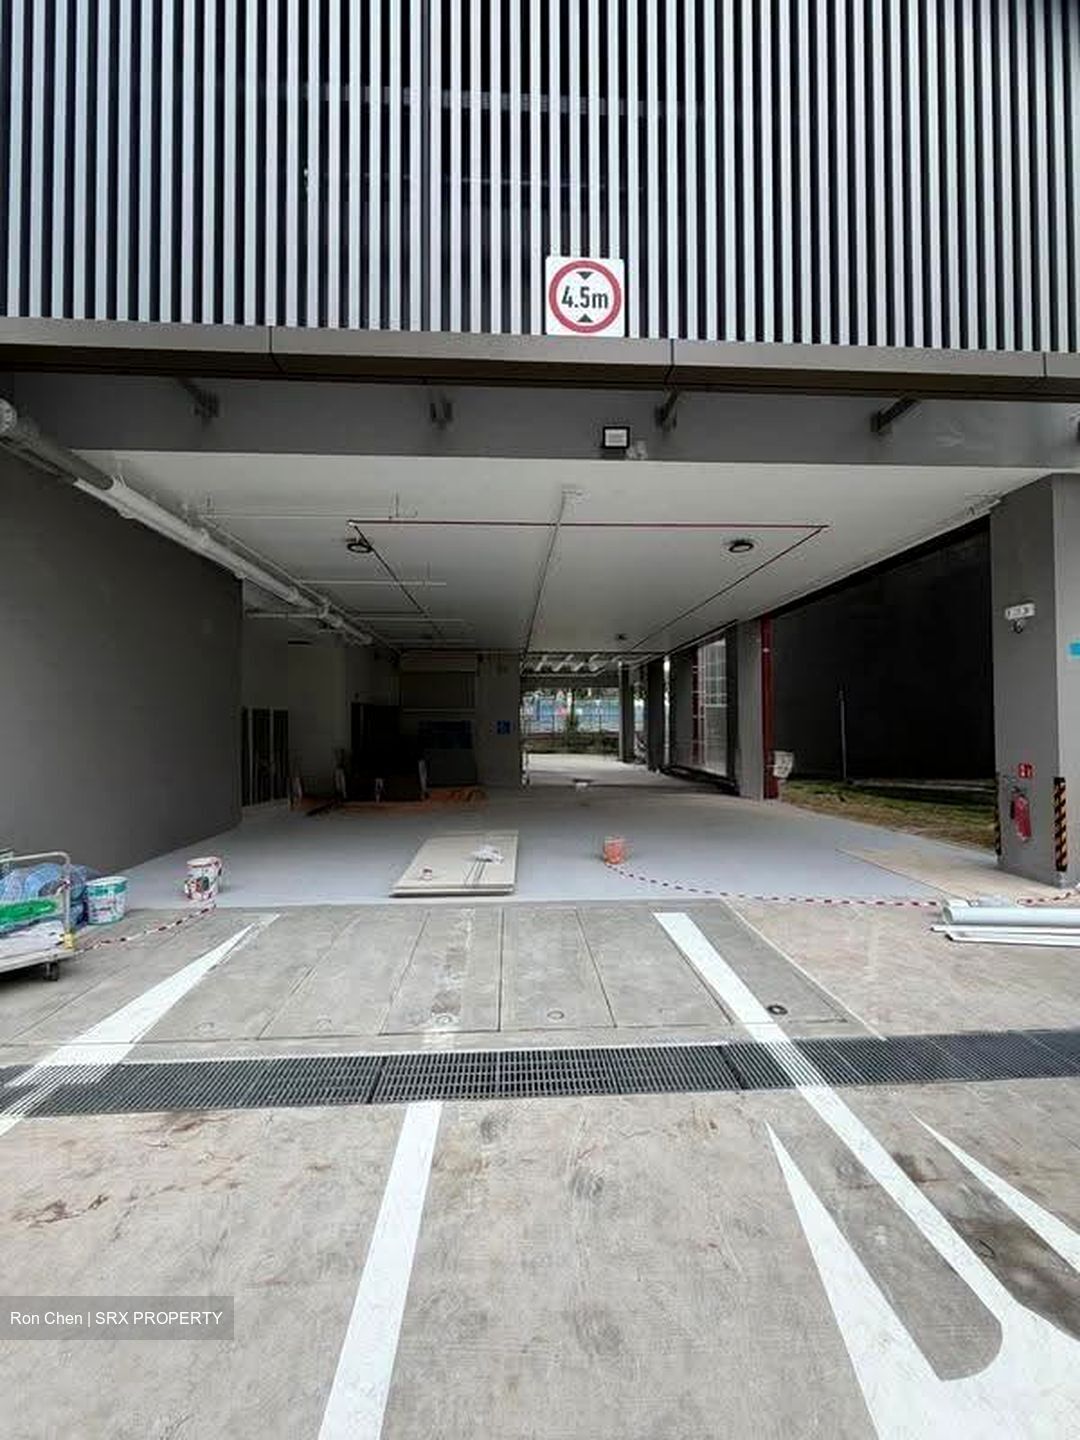
A purpose-built multi-user food manufacturing facility engineered to reduce commissioning time, minimise fit-out costs and accelerate production readiness.
⸻
Built Around How Food Manufacturers Operate
Most factories require manufacturers to adapt their production processes to the building.
This project was engineered so the building adapts to your production.
Every major design decision was made with food manufacturers in mind—from production workflow and regulatory compliance to future expansion and operational flexibility. The result is a next-generation food manufacturing facility designed to shorten fit-out timelines, reduce capital expenditure and support long-term business growth.
⸻
One Building. Multiple Brands. Multiple Production Concepts.
Unlike conventional food factories designed for a single occupier, our project has been purpose-built as a multi-user food manufacturing facility, enabling independent production operations within one integrated development.
This provides businesses with exceptional operational flexibility to:
* Operate multiple brands under one roof.
* Establish independent production environments.
* Support separate halal and non-halal production operations, subject to the relevant regulatory approvals and certification requirements.
* Expand production capacity progressively without relocating.
* Segregate production lines according to product category, customer requirements or food safety protocols.
**The building configuration also enhances operational resilience. Independent production floors may continue operating where an incident or regulatory investigation is confined to a specific occupier’s licensed production area, subject to the requirements and directions of the relevant authorities.
⸻
Engineered to Get You Into Production Faster
Every feature has been designe




 Whatsapp Chat


